

Fitting a Bearing: Methods, Tools and Common Mistakes
The good news is that fitting a bearing correctly, whichever method you use, comes down to a short set of rules: prepare the seat, match the method to the bearing's size and seat type, push or pull only on the ring that carries the interference fit, and never let force pass through the rolling elements. This guide covers each of those, and what to do when the bearing is on.
Browse our range of bearing fitting tools here
What Tools Do You Need for Fitting a Bearing?
The tools depend on the method. The two most common are mechanical (cold) and heat mounting. For mechanical mounting, you'll need a bearing fitting tool kit; for heat mounting, a bearing heater that you either buy or hire. For tapered seats on larger bearings, you'll need a hydraulic nut and pump.
Whichever method you use, wear the right PPE. SKF recommends heat-resistant gloves when handling hot bearings and oil-resistant gloves for oily ones, and safety glasses are sensible for any mounting job.
Before Fitting a Bearing - A checklist
Most bearing fitting damage is set up before the bearing is touched. Work through this checklist first:
-
Check storage. The replacement bearing should have been kept clean, dry, at ambient temperature and free from vibration.
-
Keep it wrapped. Do not unwrap the bearing until you are ready to fit it, which keeps contamination out until the last moment.
-
Inspect the shaft and housing. Both should be clean and free of gouges, nicks and burrs. Industrial Scotch-Brite pads are preferred over emery paper for removing fretting or corrosion, because loose particles from emery paper can contaminate the bearing.
-
Measure the seats. Use calibrated tools to confirm the shaft and housing are within the specified dimensional tolerances. A seat that is out of tolerance can't deliver the intended fit, whatever method you use to fit the bearing.
-
Check the lead-in. SKF recommends a 10 to 20 degree lead-in chamfer on shaft ends and housing bores, particularly on larger bearings, because without one the ring can skew during mounting and damage the mating surfaces.
-
Lubricate the mating surfaces. For an interference fit, SKF recommends a thin layer of light oil on the mating surfaces. For a loose fit, an anti-fretting agent is used instead.
Which Bearing Fitting Method Should You Use?
There are three main methods: mechanical, heat and hydraulic. The choice depends on the bearing's bore diameter and the type of seat it's going onto. SKF's size bands are small (up to 80mm bore), medium (80 to 200mm) and large (200mm and above).
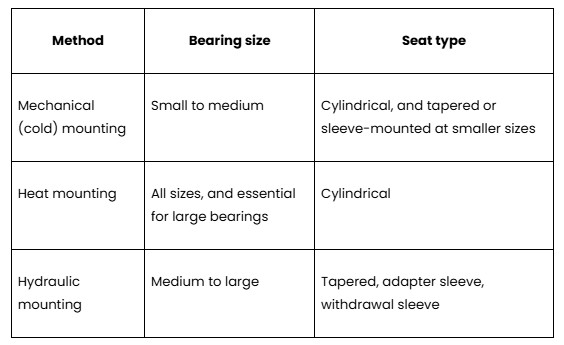
The methods overlap, so there is rarely a single correct answer. The practical rule is that the force needed to mount a bearing cold rises considerably with bearing size, which is why larger bearings generally can't be fitted cold at all. For a deeper comparison of when heat is the right call, see our guide to when to use a bearing heater.
Fitting a Bearing Mechanically
Mechanical, or cold, mounting fits a bearing without heat and suits small and medium bearings on cylindrical seats. The standard approach is to fit an impact ring to the bearing, place a sleeve on the ring, and tap the sleeve with a dead blow hammer so force travels through the impact ring and into the bearing, easing it onto the shaft without damage.
The most important rule is where the force goes. Apply it to the ring with the interference fit, which is usually the inner ring when fitting to a shaft. If a bearing must be pressed onto the shaft and into the housing at the same time, the force must be applied equally to both rings, with the tool's contact faces in the same plane. SKF also states that bearing rings, cages, rolling elements and seals must never be struck directly with a hard object.
Hammering is acceptable only with a proper fitting tool, and only on small bearings where the fit isn't too tight. Where the fit is tight, or the bearing is medium or large, a press or another method is the safer choice.
SKF's TMFT 36 fitting tool kit is a common choice for this method, supporting bearings from 10mm to 55mm bore on shaft, housing and blind applications.
Fitting a Bearing With Heat
Heating expands the bearing's inner ring, so the bore grows enough to slide onto the shaft without force. As the bearing cools, it contracts and grips the shaft, forming the interference fit. As SKF puts it, it is generally not possible to mount larger bearings without heating, because the force needed rises considerably with size.
An induction heater is the most reliable way to do it, because it heats evenly and monitors the bearing's temperature directly. Cones, hot plates and ovens are less controllable and can heat unevenly, and a naked flame should never be used because it creates local overheating that can damage the bearing steel.
Temperature limits matter as much as the method:
-
Open bearings must not be heated above 120°C.
-
Sealed or shielded bearings should not exceed 80°C, and their seals should never touch a hot plate directly.
-
A common working rule is to heat the bearing roughly 80 to 90°C above the shaft temperature, which is enough for a clean slide fit.
Once the bearing is on, hold it firmly against the shaft shoulder until it has cooled and gripped. Because the bearing also contracts axially as it cools, it can pull away from the shoulder, so a lock nut should be fitted and tightened again as the bearing cools. If you only fit bearings occasionally, hiring a heater usually costs less than buying one.
Fitting a Bearing With Hydraulics
Hydraulic methods suit bearings with tapered seats, adapter sleeves or withdrawal sleeves, where the interference fit is created by driving the bearing up a taper. The fit is set by how far the bearing travels, measured either as the reduction in radial internal clearance or as an axial drive-up distance, not by temperature or force alone.
SKF specifies the point at which hydraulics become necessary: tapered bore bearings up to 80mm bore can be driven up the seat with a fitting tool or, preferably, a lock nut, but above 80mm the force is considerable and hydraulic nuts should be used. Two hydraulic techniques are common:
The drive-up method places a hydraulic nut on the shaft thread or sleeve thread, resting against the inner ring. A hydraulic pump then pushes oil into the nut to drive the bearing up the taper. SKF recommends its Drive-up Method for medium and large bearings, because controlling axial displacement from a defined starting position gives a reliable, repeatable fit.
The oil injection method injects a thin film of oil between the bearing and its seat through ducts and grooves in the shaft, which virtually eliminates the friction between them. SKF states that when dismounting from a cylindrical seat, this can reduce the pulling force by up to 90%, and the pressures involved are typically below 100 MPa. It needs an oil duct in the shaft and a distribution groove in the seat, so it has to be designed in rather than added later.
Common Bearing Fitting Mistakes
Most failures linked to fitting a bearing come from a short list of avoidable errors:
-
Hammering the bearing directly. Force through the rolling elements, or through the loose-fit ring, can brinell the raceways, which later shows up as noise and early failure.
-
Using a naked flame. It heats unevenly and can damage the steel before the bearing is ever mounted.
-
Overheating sealed bearings. Heating a sealed bearing to open-bearing temperatures risks degrading the grease before it's in service.
-
Fitting to damaged or out-of-tolerance seats. A burr or an oversize shaft undermines any method.
-
Unwrapping the bearing early. Leaving a bearing exposed lets contamination in before it's ever fitted.
-
Skipping lubrication. With poor lubrication behind around 36% of premature failures, a perfectly fitted bearing can still fail early if it is not lubricated correctly afterwards.
Need Help With Bearing Fitting?
If you're unsure which method suits your bearing size and seat type, or you need to source fitting tools, heaters or hydraulic equipment, our bearing and maintenance experts are on hand to help. For related reading, our guide to installing bearings without damaging the shaft or housing covers the preparation stage in more detail.
Frequently Asked Questions
What is bearing fitting?
Bearing fitting, also called bearing mounting or installation, is the process of getting a bearing onto its shaft and into its housing without damaging it, so that the fit, alignment and clearance match what the application was designed for. The three main approaches are mechanical (cold) fitting, heat fitting and hydraulic fitting, chosen by bearing size and seat type.
How do you fit a bearing onto a shaft?
Prepare and measure the shaft, then choose the method by bearing size and seat type. For small and medium bearings on a cylindrical shaft, use an impact ring, sleeve and dead blow hammer or a press, applying force only to the inner ring. For larger bearings, heat the bearing with an induction heater to expand the bore, slide it on, and hold it against the shoulder as it cools. Tapered seats use a lock nut or hydraulic nut.
What is the correct way to install a bearing?
Keep the bearing wrapped until fitting, clean and inspect the shaft and housing, check they are within tolerance, then apply mounting force only to the ring with the interference fit and never through the rolling elements. Match the method to the bearing size, and lubricate correctly once it is in place.
Can you hammer a bearing on?
Only with care. A hammer should only be used on a proper fitting tool, such as an impact ring and sleeve, and only for small bearings where the fit is not too tight. Striking the bearing directly, or using a hammer on medium and large bearings or tight fits, risks damaging the raceways and shortening the bearing's life.
Which ring should you apply force to when fitting a bearing?
The ring that has the interference fit. On a rotating shaft, this is usually the inner ring. Pushing on the loose-fit ring sends force through the rolling elements and can brinell the raceways. If both rings need an interference fit, apply force to both at the same time using a tool that contacts both faces in the same plane.
How hot should you heat a bearing to fit it?
Open bearings must not exceed 120°C, and SKF does not recommend heating sealed or shielded bearings above 80°C. As a general rule, heat the bearing roughly 80 to 90°C above the shaft temperature, which is normally enough to create a clean slide fit without overheating the steel or the grease.